Inquiry
Form loading...

Alcohol Recovery Tower for Chemical Industry – Top China Suppliers & Factory for Distillation Solutions

This high-quality recovery device is ideal for the extraction of dilute alcohol in various industries, including pharmaceuticals, food, light industry, and chemical sectors. Our advanced distillation technology is also effective for purifying other soluble solvents, such as methanol. As a leading supplier based in China, our factory ensures that each unit meets rigorous quality standards, making it a reliable choice for your industrial needs. Trust our expertise as prominent suppliers in the market to provide you with efficient and durable solutions for your distillation requirements

Purpose

This device is suitable for the recovery of dilute alcohol in industries such as pharmaceuticals, food, light industry, and chemical industry. It is also suitable for distillation of other soluble coal such as methanol. This device can distill diluted alcohol at around 30 ° C to 90 ° C-95 ° C according to user needs. If the alcohol content of the finished product is higher, the reflux ratio can be increased, but the output will correspondingly decrease.

Structure and characteristics

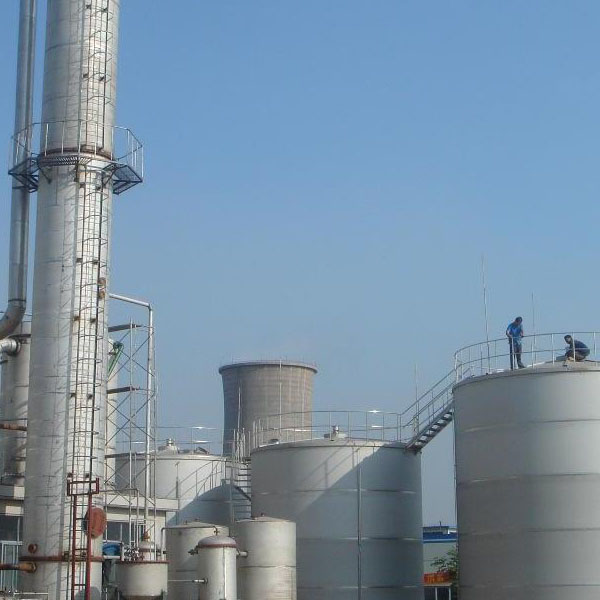
This device uses efficient metal stainless steel fillers. The distillation tower is made of stainless steel, which prevents the phenomenon of iron filings blocking the tower packing and prolongs the service life of the device. All parts of this device that come into contact with alcohol equipment, such as condensers, stabilizing tanks, cooling coils, etc., are made of stainless steel to ensure that the finished alcohol is not contaminated. The distillation kettle adopts a detachable U-shaped heating tube, which can be pulled out of the kettle during maintenance to facilitate cleaning of the outer wall of the heating tube and the distillation kettle wall. This device can be used for intermittent production, as well as semi continuous and continuous production.

Main Technical Reference Table

Item HT200 HT300 HT400 HT500 HT600 HT800
Volume(L) 640 1220 1450 2300 2500 3200
Height(mm) 6000 7000 8000 8000 10000 12000
Tank volume (L) 2300 400 650 800 1000 1500
Condenser area (㎡) 5 9 11 22 25 40
Cooling area (㎡) 1 1.5 2.2 6 8 15
Heat exchange area (㎡) 3.0 6 12 17 25 30
Ability to increase revenue(kg/h) 45-50 90-100 150-160 280-300 420-440 600-620
Recovery concentration(%) >90℃-95℃
Packing type Stainless steel corrugated packing
Weight(kg) 1100 1900 2300 3800 4500 7800
Dimension L×W×H (mm) 2300×700×7300 2600×800×7500 2500×1000×9000 3000×1200×9000 3500×1400×9000 4200×1800×1400

Working principle

The working principle of the alcohol recovery tower utilizes the principle that the boiling point of alcohol is lower than that of other solutions. A temperature slightly higher than the boiling point of alcohol is used to heat and evaporate the dilute alcohol solution that needs to be recovered. After being refined by the tower body, pure alcohol gas is precipitated to increase the concentration of the alcohol solution and achieve the goal of recovering alcohol.

Frequently Asked Questions

What industries is this recovery device suitable for?

This device is suitable for the recovery of dilute alcohol in industries such as pharmaceuticals, food, light industry, and chemical industry. It is also suitable for the distillation of other soluble coal such as methanol.

What temperature range does this distillation process operate in?

The device can distill diluted alcohol at around 30 °C to 90 °C-95 °C according to user needs.

How does the device prevent contamination of the finished alcohol?

All parts of the device that come into contact with alcohol, such as the distillation tower, condensers, stabilizing tanks, and cooling coils, are made of stainless steel to ensure the finished product is not contaminated.

What are the benefits of the detachable U-shaped heating tube?

The U-shaped heating tube can be pulled out of the kettle during maintenance, which facilitates easy cleaning of both the outer wall of the heating tube and the inner wall of the distillation kettle.

Does this system support continuous production?

Yes, this device is versatile and can be used for intermittent production, as well as semi-continuous and continuous production processes.

How does the reflux ratio affect the output concentration and volume?

If the alcohol content of the finished product needs to be higher, the reflux ratio can be increased. However, this will cause the output volume to decrease correspondingly.