

China Alcohol Recovery Tower for Chemical Industry - Leading Suppliers & Factory Solutions for Dilute Alcohol Recovery
Purpose
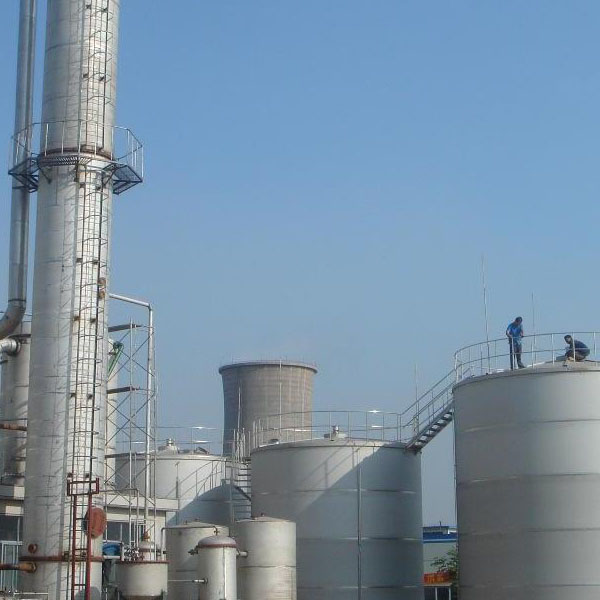
This device is suitable for the recovery of dilute alcohol in industries such as pharmaceuticals, food, light industry, and chemical industry. It is also suitable for distillation of other soluble coal such as methanol. This device can distill diluted alcohol at around 30 ° C to 90 ° C-95 ° C according to user needs. If the alcohol content of the finished product is higher, the reflux ratio can be increased, but the output will correspondingly decrease.
Structure and characteristics
This device uses efficient metal stainless steel fillers. The distillation tower is made of stainless steel, which prevents the phenomenon of iron filings blocking the tower packing and prolongs the service life of the device. All parts of this device that come into contact with alcohol equipment, such as condensers, stabilizing tanks, cooling coils, etc., are made of stainless steel to ensure that the finished alcohol is not contaminated.
The distillation kettle adopts a detachable U-shaped heating tube, which can be pulled out of the kettle during maintenance to facilitate cleaning of the outer wall of the heating tube and the distillation kettle wall. This device can be used for intermittent production, as well as semi continuous and continuous production.
Main technical reference table
Item |
HT200 |
HT300 |
HT400 |
HT500 |
HT600 |
HT800 |
Volume(L) |
640 |
1220 |
1450 |
2300 |
2500 |
3200 |
Height(mm) |
6000 |
7000 |
8000 |
8000 |
10000 |
12000 |
Tank volume (L) |
2300 |
400 |
650 |
800 |
1000 |
1500 |
Condenser area (㎡) |
5 |
9 |
11 |
22 |
25 |
40 |
Cooling area (㎡) |
1 |
1.5 |
2.2 |
6 |
8 |
15 |
Heat exchange area (㎡) |
3.0 |
6 |
12 |
17 |
25 |
30 |
Ability to increase revenue(kg/h) |
45-50 |
90-100 |
150-160 |
280-300 |
420-440 |
600-620 |
Recovery concentration(%) |
>90℃-95℃ |
|||||
Packing type |
Stainless steel corrugated packing |
|||||
Weight(kg) |
1100 |
1900 |
2300 |
3800 |
4500 |
7800 |
Dimension L×W×H (mm) |
2300×700×7300 |
2600×800×7500 |
2500×1000×9000 |
3000×1200×9000 |
3500×1400×9000 |
4200×1800×1400 |
Working principle
The working principle of the alcohol recovery tower utilizes the principle that the boiling point of alcohol is lower than that of other solutions. A temperature slightly higher than the boiling point of alcohol is used to heat and evaporate the dilute alcohol solution that needs to be recovered. After being refined by the tower body, pure alcohol gas is precipitated to increase the concentration of the alcohol solution and achieve the goal of recovering alcohol.
Frequently Asked Questions
Q: What industries is this alcohol recovery device suitable for?
This device is highly suitable for recovering dilute alcohol in industries such as pharmaceuticals, food, light industry, and chemical processing. It is also designed for the distillation of other soluble solvents like methanol.
Q: What materials are used to construct the recovery system?
To ensure the finished alcohol is not contaminated, all parts that come into contact with alcohol (such as the distillation tower, condensers, stabilizing tanks, and cooling coils) are made of high-quality stainless steel.
Q: How does the detachable heating tube design benefit maintenance?
The distillation kettle features a detachable U-shaped heating tube. During maintenance, this tube can be pulled completely out of the kettle, facilitating easy cleaning of both the outer wall of the heating tube and the inner wall of the distillation kettle.
Q: Can this device be used for continuous production?
Yes, this device is highly versatile and can be configured for intermittent production, semi-continuous production, as well as fully continuous production processes.
Q: What is the primary working principle of the alcohol recovery tower?
It operates on the principle that alcohol has a lower boiling point than other solutions. By heating the dilute alcohol solution to a temperature slightly higher than the boiling point of alcohol, the alcohol evaporates, is refined through the tower body, and precipitates as pure alcohol gas.
Q: How can I achieve a higher alcohol concentration in the finished product?
To obtain a higher alcohol content, you can increase the reflux ratio of the distillation process. However, please note that increasing the reflux ratio will correspondingly decrease the overall output volume.