

China Suppliers Alcohol Recovery Tower for Chemical Industry - Efficient Distillation Factory Equipment
Purpose
This device is suitable for the recovery of dilute alcohol in industries such as pharmaceuticals, food, light industry, and chemical industry. It is also suitable for distillation of other soluble coal such as methanol. This device can distill diluted alcohol at around 30 ° C to 90 ° C-95 ° C according to user needs. If the alcohol content of the finished product is higher, the reflux ratio can be increased, but the output will correspondingly decrease.
Structure and characteristics
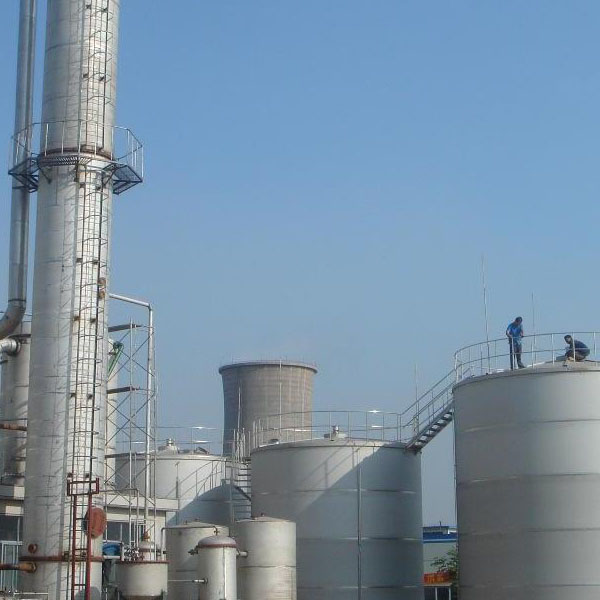
This device uses efficient metal stainless steel fillers. The distillation tower is made of stainless steel, which prevents the phenomenon of iron filings blocking the tower packing and prolongs the service life of the device. All parts of this device that come into contact with alcohol equipment, such as condensers, stabilizing tanks, cooling coils, etc., are made of stainless steel to ensure that the finished alcohol is not contaminated. The distillation kettle adopts a detachable U-shaped heating tube, which can be pulled out of the kettle during maintenance to facilitate cleaning of the outer wall of the heating tube and the distillation kettle wall. This device can be used for intermittent production, as well as semi continuous and continuous production.
Main technical reference table
| Item | HT200 | HT300 | HT400 | HT500 | HT600 | HT800 |
| Volume(L) | 640 | 1220 | 1450 | 2300 | 2500 | 3200 |
| Height(mm) | 6000 | 7000 | 8000 | 8000 | 10000 | 12000 |
| Tank volume (L) | 2300 | 400 | 650 | 800 | 1000 | 1500 |
| Condenser area (㎡) | 5 | 9 | 11 | 22 | 25 | 40 |
| Cooling area (㎡) | 1 | 1.5 | 2.2 | 6 | 8 | 15 |
| Heat exchange area (㎡) | 3.0 | 6 | 12 | 17 | 25 | 30 |
| Ability to increase revenue(kg/h) | 45-50 | 90-100 | 150-160 | 280-300 | 420-440 | 600-620 |
| Recovery concentration(%) | >90℃-95℃ | |||||
| Packing type | Stainless steel corrugated packing | |||||
| Weight(kg) | 1100 | 1900 | 2300 | 3800 | 4500 | 7800 |
| Dimension L×W×H (mm) | 2300×700×7300 | 2600×800×7500 | 2500×1000×9000 | 3000×1200×9000 | 3500×1400×9000 | 4200×1800×1400 |
Working principle
The working principle of the alcohol recovery tower utilizes the principle that the boiling point of alcohol is lower than that of other solutions. A temperature slightly higher than the boiling point of alcohol is used to heat and evaporate the dilute alcohol solution that needs to be recovered. After being refined by the tower body, pure alcohol gas is precipitated to increase the concentration of the alcohol solution and achieve the goal of recovering alcohol.
Frequently Asked Questions (FAQ)
This device is suitable for recovering dilute alcohol in industries such as pharmaceuticals, food, light industry, and chemical industry. It is also designed for the distillation of other soluble coal like methanol.
According to user needs, the device can distill diluted alcohol at around 30 °C to 90 °C-95 °C. Increasing the reflux ratio can result in higher alcohol content, though the output will decrease correspondingly.
The distillation tower uses efficient metal stainless steel fillers. All parts in contact with alcohol—including condensers, stabilizing tanks, and cooling coils—are constructed of stainless steel to ensure the finished alcohol remains uncontaminated.
The distillation kettle features a detachable U-shaped heating tube. This design allows it to be pulled out of the kettle during maintenance, making it easy to clean the outer wall of the heating tube and the inner wall of the distillation kettle.
This device is highly versatile and can be utilized for intermittent production, as well as semi-continuous and continuous production processes.
It works based on the principle that alcohol has a lower boiling point than other solutions. By applying a temperature slightly higher than alcohol's boiling point, the dilute solution evaporates. The vapor is then refined in the tower body, precipitating pure alcohol gas to increase the overall solution concentration.