

China Suppliers Alcohol Recovery Tower for Chemical Industry - Efficient Distillation for Pharmaceuticals & Food Factory
Purpose
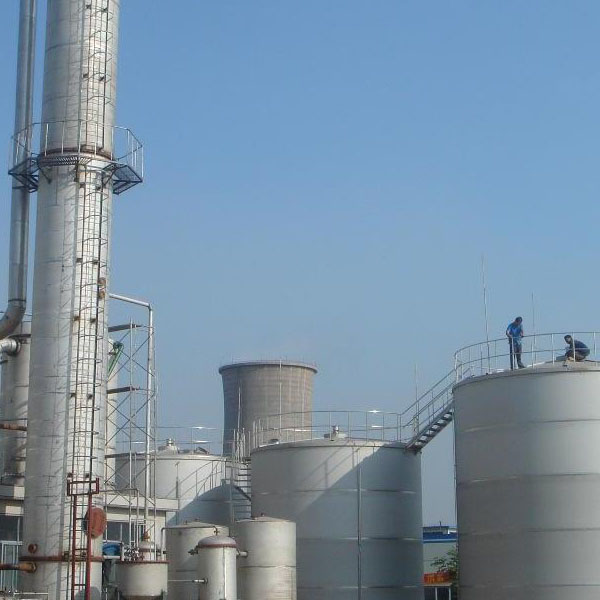
Structure and characteristics
Main technical reference table
| Item | HT200 | HT300 | HT400 | HT500 | HT600 | HT800 |
| Volume(L) | 640 | 1220 | 1450 | 2300 | 2500 | 3200 |
| Height(mm) | 6000 | 7000 | 8000 | 8000 | 10000 | 12000 |
| Tank volume (L) | 2300 | 400 | 650 | 800 | 1000 | 1500 |
| Condenser area (㎡) | 5 | 9 | 11 | 22 | 25 | 40 |
| Cooling area (㎡) | 1 | 1.5 | 2.2 | 6 | 8 | 15 |
| Heat exchange area (㎡) | 3.0 | 6 | 12 | 17 | 25 | 30 |
| Ability to increase revenue(kg/h) | 45-50 | 90-100 | 150-160 | 280-300 | 420-440 | 600-620 |
| Recovery concentration(%) | >90℃-95℃ | |||||
| Packing type | Stainless steel corrugated packing | |||||
| Weight(kg) | 1100 | 1900 | 2300 | 3800 | 4500 | 7800 |
| Dimension L×W×H (mm) | 2300×700×7300 | 2600×800×7500 | 2500×1000×9000 | 3000×1200×9000 | 3500×1400×9000 | 4200×1800×14000 |
Working principle
Frequently Asked Questions (FAQ)
What industries and materials is this alcohol recovery device suitable for?
This device is suitable for recovering dilute alcohol in industries such as pharmaceuticals, food, light industry, and chemical industries. It is also highly suitable for the distillation of other soluble coal solutions, such as methanol.
How does the design prevent contamination of the finished alcohol?
All parts of the device that come into direct contact with alcohol—including the condensers, stabilizing tanks, and cooling coils—are constructed from stainless steel. This design ensures that the finished alcohol remains uncontaminated and prevents iron filings from blocking the tower packing.
What are the benefits of the detachable U-shaped heating tube?
The distillation kettle utilizes a detachable U-shaped heating tube that can be completely pulled out of the kettle during maintenance. This feature significantly facilitates the easy cleaning of both the outer wall of the heating tube and the inner wall of the distillation kettle.
Can this device support different types of production modes?
Yes, this recovery device is highly versatile and can be configured for intermittent production, semi-continuous production, and fully continuous production depending on operational requirements.
How does the reflux ratio affect the output and concentration of alcohol?
If a higher alcohol concentration is required in the finished product, the reflux ratio can be increased. However, increasing the reflux ratio will result in a corresponding decrease in the overall output volume.
What is the core working principle of the alcohol recovery tower?
The system utilizes the difference in boiling points between alcohol and other solutions. By heating the dilute alcohol solution to a temperature slightly higher than the boiling point of alcohol, the alcohol evaporates. The vapor is then refined by the tower body to precipitate pure alcohol gas and increase the concentration.