

China Suppliers of Packed Towers with Liquid Distributors for Enhanced Separation Performance - Factory Direct Solutions
Description
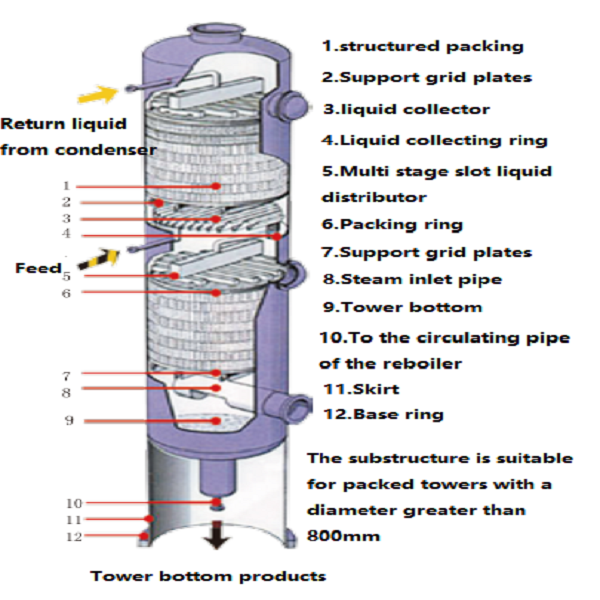
The separation performance of a structured packing tower depends on the internal components, such as packing, distributors, collectors, etc. It also depends on many parameters, such as gas load, liquid load, material properties, operating pressure, packing wetting performance, and uneven liquid distribution. Until now, it is not possible to accurately calculate the separation performance of the tower based on the geometric shape of the packing, and accurate data needs to be determined through the theory of packing towers and experimental towers under different conditions. Users can approximate the size of the tower and the required filling height based on the data.
Application Area
With the continuous development and application of new tower fillers, the advantages of packed towers have become more prominent and their application scope is expanding. The applications in the refining, petrochemical, fine chemical, fertilizer, pharmaceutical, and atomic energy industries, as well as in the field of environmental protection, have become more mature. Packing towers are particularly suitable for vacuum distillation, atmospheric and medium pressure distillation, as well as two-phase contact processes with atmospheric volume (such as gas absorption, cooling, etc.), but special caution should be exercised when applying them in high-pressure distillation towers. People are conducting research on high-pressure distillation packing towers, attempting to solve the problem from the structure and operation methods of packing towers, such as proposing segmented emulsification of packing layers or using high gravity field separation. Some progress has been made in breaking through the limitations of using fillers in high-pressure distillation columns, and the key is to thoroughly understand the impact of high pressure (high liquid phase load) on the processing capacity and efficiency of the tower. Shallow bed and high-performance tower components (such as gas distributors, liquid distributors, and re distributors) can be utilized. Some people also suggest developing composite fillers suitable for high-pressure distillation.
Another new field of application for packed towers is air separation devices. Before the 1930s, air separation equipment was mainly used for welding, cutting oxygen, and chemical nitrogen. Due to the development of modern technologies such as steel, nitrogen fertilizers, chemicals, and rockets, the usage of oxygen, nitrogen, and rare gases has rapidly increased. Some large foreign companies, such as Linde in Germany, APCI (Air Products and Chemicals) in the United States, BOC (Oxygen) in the United Kingdom, and Air Liquefaction in France, have started to apply packed towers to air separation research. Sulzer in Switzerland, as a packing manufacturer, actively cooperates with these companies and has achieved gratifying results.
Another use of regular fillers in air separation units is in crude argon towers. The previous crude argon tower was a sieve plate tower, which could not obtain pure argon with an oxygen content less than 2 × 10⁻⁶. By switching to a packed tower, the downstream processes used in the production of pure argon products in the past can be eliminated.
Frequently Asked Questions
Q1 What factors determine the separation performance of a structured packing tower?
The separation performance depends on internal components such as packing, distributors, and collectors, as well as parameters like gas load, liquid load, material properties, operating pressure, packing wetting performance, and liquid distribution uniformity.
Q2 Which industries commonly apply packed towers?
Packed towers are maturely applied in the refining, petrochemical, fine chemical, fertilizer, pharmaceutical, atomic energy, and environmental protection industries.
Q3 What processes are packed towers most suitable for?
They are highly suitable for vacuum distillation, atmospheric and medium pressure distillation, and two-phase contact processes with atmospheric volume, such as gas absorption and cooling.
Q4 How are researchers addressing the limitations of packed towers in high-pressure distillation?
Researchers are studying segmented emulsification of packing layers, high gravity field separation, shallow beds, high-performance tower components (gas/liquid distributors and redistributors), and composite fillers to handle high liquid phase loads.
Q5 What is the advantage of using packed towers in crude argon recovery?
By replacing traditional sieve plate towers with packed towers, systems can obtain pure argon with an oxygen content of less than 2 × 10⁻⁶, successfully eliminating the need for previous downstream purification processes.